new blog
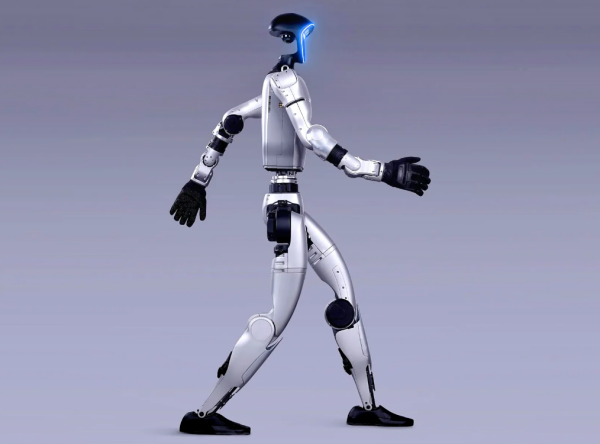
A humanoid robot can contain hundreds of structural and transmission components. Across the industry, two material-selection mistakes keep appearing—and both can be costly:
Saving on specialty materials when they are actually needed
—For example, using PA66-GF30 for a bracket near a motor can lead to creep deformation, dimensional changes, and position drift under prolonged high-temperature exposure.
Using specialty materials where they are not actually necessary
—For example, using PEEK for a non-load-bearing housing. The material performance is excessive for the application, while the BOM cost can increase dramatically.
PPA (polyphthalamide), commonly known as high-temperature nylon, sits right between these two extremes. It is neither simply “more expensive nylon” nor “cheaper PEEK.” It has its own clearly defined position in material selection.
This article explains exactly where PPA fits: which components are a good match for PPA, where using it would be an over-specification, as well as its processing window and key validation requirements.
PPA is a semi-aromatic polyamide. Unlike conventional nylons such as PA6 and PA66, which have predominantly aliphatic molecular chains, PPA incorporates aromatic diacid segments, such as terephthalic acid and isophthalic acid.
The rigid benzene rings and lower density of polar groups lead to three simultaneous changes:
| Property | PA66 | PPA-LGF | Trend |
|---|---|---|---|
| Melting point | Around 260°C | 320–350°C | Significantly higher |
| Long-term service temperature | Approx. 100–120°C | 150–180°C | Increased by 30–50°C |
| HDT (1.82 MPa) | Approx. 240–250°C | 308°C | Increased |
| Equilibrium water absorption (23°C / 50% RH) | Approx. 2% | Approx. 0.3% | Reduced to about 1/4 |
| Moisture content before processing | ≤0.20% | ≤0.01% | Much stricter requirement |
Based on operating conditions, PPA offers four key high-value application areas:
The continuous operating temperature around motors is typically in the range of 80–120°C. Conventional reinforced nylons can experience creep and dimensional drift during long-term operation in this temperature range, while the positioning accuracy of sensor brackets directly affects calibration results.
With its high HDT and low water absorption, PPA is a suitable material choice for these applications.
One of the most established applications for PPA is SMT connectors. The material must withstand lead-free reflow soldering, where peak temperatures can reach around 260°C, without blistering or deformation. After soldering, it must also maintain stable contact spacing in humid environments.
The same requirements apply to connectors, high-voltage connectors, and PCB support components inside a robot's electronic control compartment.
This has been one of the fastest-growing application areas for PPA in recent years. Long-glass-fiber-reinforced PPA can reach tensile strength levels above 240 MPa, with a density of approximately 1.56 g/cm³, making it roughly 40% lighter than aluminum based on density comparison.
The key value is not simply absolute strength, but the chain of benefits that comes from reducing weight and, in turn, lowering the load on the motor.
Dexterous hand actuators typically have short strokes, high reciprocating frequencies, and tight clearance requirements. This places simultaneous demands on wear resistance and dimensional stability.
For these components, material selection should use dimensional retention after repeated reciprocating cycles as a key evaluation criterion, rather than relying solely on initial material properties.
This is where PPA is most easily misused. Reinforced PPA offers high strength and stiffness, but it does not have inherent self-lubricating properties. Its wear resistance and coefficient of friction are generally less favorable than those of PEEK or POM.
If PPA is selected for friction pairs inside a joint—such as bearings, gear meshing surfaces, or bushings—simply on the assumption that “the strength is sufficient,” wear and clearance growth can occur relatively quickly.
Friction interfaces are better served by PEEK or PEEK+PTFE systems, while POM can be considered for lightly loaded, low-noise components. PPA belongs in load-bearing structures, not at the friction interface.
PPA has a much lower water absorption rate than PA66, but it is not moisture-proof. A water absorption rate of 0.3–0.5% corresponds to a dimensional change of approximately 0.15–0.25 mm over a 50 mm span (engineering estimate, assuming proportional dimensional change).
For applications such as joint mating components and gear center distances, this level of dimensional change can be enough to consume the available assembly clearance.
The price gap between PEEK and PPA can be several-fold. The cost-saving logic of tiered material selection is to reserve PEEK for applications where it is truly necessary, rather than replacing it across the board.
PPA has a much narrower processing window than PA66. Even with the same grade, different processing conditions can result in parts with significantly different performance.
| Process | Control Direction | Consequences of Poor Control |
|---|---|---|
| Drying | Dehumidifying drying is essential. Moisture content must be reduced to a very low level, much stricter than for PA66, with a dew point around −40°C. | Hydrolytic chain scission at high temperatures → brittle parts, silver streaks, and bubbles |
| Melt Temperature | Higher than that of conventional nylon; set according to the specific material system and do not exceed the recommended upper limit. | Too low → insufficient plasticization; too high → thermo-oxidative degradation and discoloration |
| Residence Time | Keep it as short as possible, with control on a minute scale. | Molecular weight reduction and black specks |
| Mold Temperature | High mold temperature is a prerequisite, especially for precision components. | Low mold temperature → insufficient crystallinity → post-shrinkage, warpage, dimensional drift, and poor surface gloss |
| Holding Pressure | Keep within the appropriate mid-range according to wall thickness and avoid over-packing. | Too high → residual stress; too low → sink marks and voids |
| Annealing | Stress-relief annealing after molding is recommended for precision components. | Residual internal stress → gradual deformation after assembly |
| Regrind | Control the regrind ratio and thoroughly dry the material again before processing. | Cumulative molecular weight reduction; not recommended for critical reliability components |
For semi-crystalline materials, crystallinity is strongly influenced by mold temperature. A part molded at too low a mold temperature may look fine after demolding, but its dimensions can continue to change after assembly.
Many complaints about "PPA dimensional instability" actually originate from insufficient mold temperature rather than material lot variation.
After glass-fiber or carbon-fiber reinforcement, the difference in shrinkage between the flow direction and the transverse direction can become significant. Fiber orientation is also affected by gate location and shear rate.
For these components, mold-flow analysis should be carried out and appropriate shrinkage compensation should be incorporated into the mold design. Simply adjusting the molding parameters may not be enough to bring the part back within tolerance.
follow us :


-- get updates with latest topics
 e-mail
 English
 français
 Deutsch
 русский
 italiano
 español
 português
 العربية
 日本語
 한국의
 中文